Stainless steel passivation helps protect CNC machined parts from rust caused by iron contamination left on the surface during manufacturing. Although stainless steel naturally resists corrosion, traces of iron introduced during machining or handling can rust when exposed to moisture.
For parts such as valve bodies, fittings, shafts, and equipment housings exposed to moisture or repeated cleaning, passivation can be an important finishing step. Its effectiveness depends on the stainless steel grade, proper surface cleaning, and a treatment suited to the part.
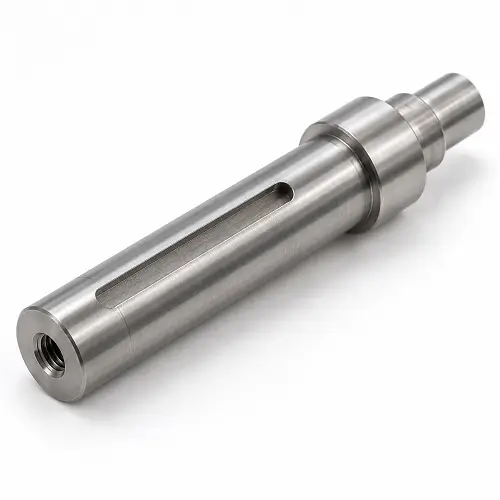
What Is Stainless Steel Passivation?
Stainless steel passivation is a chemical treatment that removes free iron contamination from the surface and helps the metal maintain its natural corrosion resistance. After cleaning away machining oils and residue, the parts undergo a suitable acid treatment, followed by thorough rinsing and drying.
“Free iron” refers to iron contamination on the surface, rather than the iron that belongs in the stainless steel alloy. Removing this contamination helps the stainless steel form and maintain its thin, protective oxide film.
Passivated stainless steel does not have an added metallic coating like a nickel-plated part. It usually looks much the same as before treatment. The purpose is to reduce contamination-related corrosion, rather than make the surface shinier or smoother.
Why Can Stainless Steel Rust After Machining?
Stainless steel gets much of its corrosion resistance from a chromium-rich passive film that forms naturally on a clean surface exposed to oxygen. Machining exposes fresh metal, but that does not permanently remove its protection—the film can form again.
The problem is what may remain on that fresh surface. Iron-contaminated abrasives, tools, or handling equipment can transfer particles onto the part. Those particles may be too small to see during visual inspection, yet produce orange rust spots when moisture reaches them.
Consider a stainless steel fitting that looks clean after turning but develops spots during storage. The spots do not automatically prove that the wrong material was used. Surface contamination, packaging conditions, and moisture exposure also need investigation.
Simply wiping away the discoloration leaves the cause uncertain. If contamination is responsible, cleaning and an appropriate passivation process can address it. If the stainless steel itself is corroding because the environment is too aggressive, the material or application needs further review.
When Is Passivation of Stainless Steel Required?
The drawing and purchase specification come first. When passivation is specified, a clean appearance is not a reason to omit it.
When the treatment is optional, consider where the part will operate. A spacer inside a dry enclosure has different exposure from a valve component that handles liquid or a fitting that is washed repeatedly. Moisture and cleaning chemicals make the surface condition more consequential.
For example, a stainless steel component used in washdown equipment may remain wet around joints or recesses. Reviewing its material, surface treatment, and drainage before production is more useful than waiting for discoloration to appear after installation.
Passivation does not make every stainless steel grade suitable for every environment. A component exposed to aggressive chemicals or chlorides may still corrode after treatment. Choosing the correct alloy remains necessary.
For a low-exposure internal component with no specified passivation requirement, discuss whether the treatment provides a useful benefit
Stainless Steel Passivation: Why Do Machined Parts Need It?
Stainless steel passivation helps protect CNC machined parts from rust caused by iron contamination left on the surface during manufacturing. Although stainless steel naturally resists corrosion, traces of iron introduced during machining or handling can rust when exposed to moisture.
For parts such as valve bodies, fittings, shafts, and equipment housings exposed to moisture or repeated cleaning, passivation can be an important finishing step. Its effectiveness depends on the stainless steel grade, proper surface cleaning, and a treatment suited to the part.
What Is Stainless Steel Passivation?
Stainless steel passivation is a chemical treatment that removes free iron contamination from the surface and helps the metal maintain its natural corrosion resistance. After machining oils and residue are cleaned away, the parts undergo a suitable acid treatment, followed by thorough rinsing and drying.
“Free iron” refers to iron contamination on the surface, rather than the iron that belongs in the stainless steel alloy. Removing this contamination helps the surface develop and maintain its thin, protective oxide film.
Passivated stainless steel does not have an added metallic coating like a nickel-plated part. It usually looks much the same as before treatment. The purpose is to reduce contamination-related corrosion, rather than make the surface shinier or smoother.
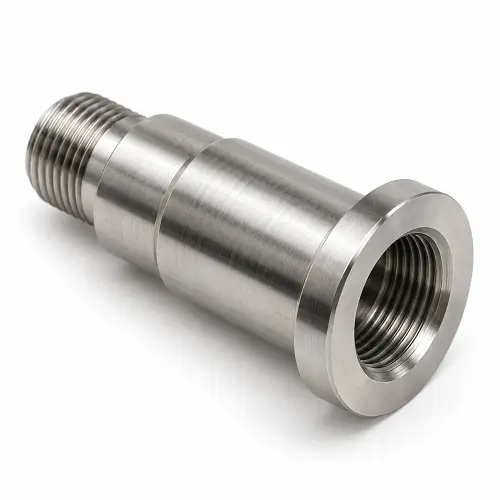
Why Can Stainless Steel Rust After Machining?
Stainless steel naturally forms a chromium-rich passive film when its clean surface is exposed to oxygen. Machining exposes fresh metal, but the protective film can form again. Cutting the material does not permanently remove its ability to resist corrosion.
Problems can arise when manufacturing leaves contamination behind. Shared abrasives, iron-contaminated handling equipment, and other shop contact can transfer particles onto the finished part. Those particles may be invisible during inspection but produce orange rust spots after exposure to moisture.
For example, a machined fitting that develops spots during storage may have surface contamination rather than an incorrect material grade. However, appearance alone cannot establish the cause. The material, manufacturing process, packaging, and storage conditions all need checking.
Wiping away the stain may improve its appearance without solving the problem. If contamination remains, the spots can return. Cleaning and passivation can address that contamination, while changes to handling and packaging help prevent it from being introduced again.
When Is Passivation of Stainless Steel Required?
A drawing or purchase specification that requires passivation makes the decision straightforward: the treatment belongs in the manufacturing plan, even when the finished parts look clean.
When no treatment is specified, the operating environment provides a useful starting point. A spacer inside a dry enclosure has different exposure from a valve component that contacts liquid or a bracket that is washed regularly. Moisture, cleaning chemicals, and the consequences of rust help determine whether passivation should be included.
Consider a stainless steel fitting in equipment that undergoes frequent cleaning. Surface contamination could create rust spots despite the fitting being made from the specified alloy. Reviewing passivation before production is more useful than waiting for discoloration to appear after assembly.
However, passivation cannot compensate for an unsuitable material. If a component repeatedly pits in a particular chemical or chloride-containing environment, the alloy and service conditions need review. Repeating the treatment will not turn that grade into a more corrosion-resistant alloy.
For parts with mild exposure and no treatment requirement, passivation should be evaluated rather than automatically added to every order. The decision should reflect how the component will be used and what level of corrosion performance is required.
How Are Stainless Steel Parts Passivated After CNC Machining?
The process begins with cleaning. Cutting fluid, grease, and debris must be removed before the passivation solution can reach the metal surface. Placing an oily part directly into a treatment bath does not reliably combine cleaning and passivation into one operation.
The cleaned parts undergo an appropriate chemical treatment, followed by thorough rinsing and drying. Citric acid passivation and nitric acid passivation are both established methods. The selected process must suit the stainless steel grade and the drawing requirements.
A material description of “stainless steel” is therefore not enough. Free-machining grades such as 303 need particular attention because their sulfur-containing inclusions affect how the surface responds. A treatment used successfully on one alloy should not automatically be applied to another.
Geometry matters as well. A simple shaft is easier to clean and rinse than a valve body with blind holes and intersecting passages. Those internal features need effective solution access and drainage so machining residue or treatment chemicals are not left inside.
Passivation is generally planned after machining, deburring, and other operations that could contaminate the finished surface. If a hole is drilled or a face is reworked afterward, the supplier should review whether cleaning and passivation need to be repeated.
Does Passivation Affect Dimensions, Threads, or Surface Finish?
A precision bore raises an understandable concern: will treatment make it too small for the mating shaft?
Proper chemical passivation does not build up a deposited coating. A bore normally does not need the coating allowance associated with nickel plating, and threads do not normally need to be cut oversize to accommodate passivation. The process is intended to preserve the finished dimensions and surface condition.
The complete finishing sequence still matters. If the part also needs pickling, abrasive cleaning, or electropolishing, those operations may remove material or change surface texture. A quotation that groups every operation under “surface treatment” can hide this distinction.
For a close-fitting sleeve, identify the bore as a final acceptance dimension and confirm which operations occur before inspection. Do not change the machining size merely because passivation appears on the drawing.
Unexpected etching, pitting, or dimensional change after treatment should be investigated. It should not be accepted as a normal result of properly controlled passivation.
Does Passivation Remove Rust, Tool Marks, or Weld Discoloration?
A rust stain, a machining groove, and a heat-tinted weld are different problems. Passivation should not be expected to fix all three.
Light contamination-related rust may be addressed through a suitable cleaning and passivation sequence. Existing corrosion pits are different: removing the corrosion products does not replace the metal already lost. A cleaned pit on a sealing face may still cause leakage or fail the drawing requirements.
Tool marks and scratches also remain unless another finishing operation removes them. If a sealing surface needs lower roughness, specify the required surface finish so the machining or polishing process can produce it before final treatment.
| Surface problem | What needs attention |
|---|---|
| Rust spots associated with iron contamination | Cleaning, contamination removal, and suitable passivation |
| Existing corrosion pits | Remaining damage and whether the part still meets functional requirements |
| Tool marks or scratches | Machining, grinding, or polishing |
| Weld heat tint or oxide scale | An appropriate oxide-removal process |
| Sharp edges or machining burrs | Deburring before final treatment |
For a component that is both welded and machined, include that information when discussing finishing. A passivation process intended for clean machined surfaces should not be assumed to remove weld scale.
Passivation vs. Electropolishing: Which Does the Part Need?
Consider a turned spacer whose dimensions and surface finish already meet the drawing. If the remaining concern is free iron contamination, passivation may address the requirement without deliberately removing a layer of base metal.
A fluid-contact component with a rougher surface presents a different problem. Electropolishing may be worth evaluating when the goal includes smoothing microscopic surface peaks and improving cleanability. It removes a controlled amount of metal, so the process must be considered alongside the final dimensional requirements.
That difference matters for small threads, precision bores, and sharp edges. Electropolishing cannot always be substituted for passivation without reviewing how material removal will affect the part.
When specifying surface finishing, describe the result that matters: contamination removal, a particular roughness, cleanability, or appearance. “Make it shiny and corrosion-resistant” leaves the supplier guessing about which requirements take priority.
How Can Passivation Be Specified and Verified?
A drawing note that says only “passivate” may leave the treatment and acceptance requirements open to interpretation. Identify the applicable specification and revision, together with any required method, testing, and documentation. ASTM A967/A967M is one specification used for chemical passivation of stainless steel parts.
If the customer has not selected a treatment method, the supplier can propose one for review based on the alloy and applicable requirements. The method should be agreed upon before production rather than chosen after the parts are finished.
Appearance alone cannot confirm successful passivation. A part may look bright while still carrying contamination. The required acceptance test should be appropriate for the stainless steel grade and specification; different tests are not automatically interchangeable.
Where documentation is required, request records tied to the supplied batch, identifying the treatment and required test results. A general statement that a supplier offers passivation does not establish how a particular shipment was processed.
Clean handling after treatment also matters. Putting finished parts back onto contaminated equipment can reintroduce the problem. Packaging should protect the cleaned surface through storage and delivery.
CNC Machined Stainless Steel Parts with Passivation
For stainless steel shafts, fittings, housings, and valve components, machining and passivation should be planned together. The alloy must suit the operating environment, the finished dimensions must support assembly, and the surface treatment must address the actual contamination or corrosion concern.
Send JeekRapid the drawing, material grade, quantity, and any passivation requirements for a CNC machining quote. If the treatment is undecided, include the operating environment and cleaning chemicals the part will encounter so the machining and finishing requirements can be reviewed together.